
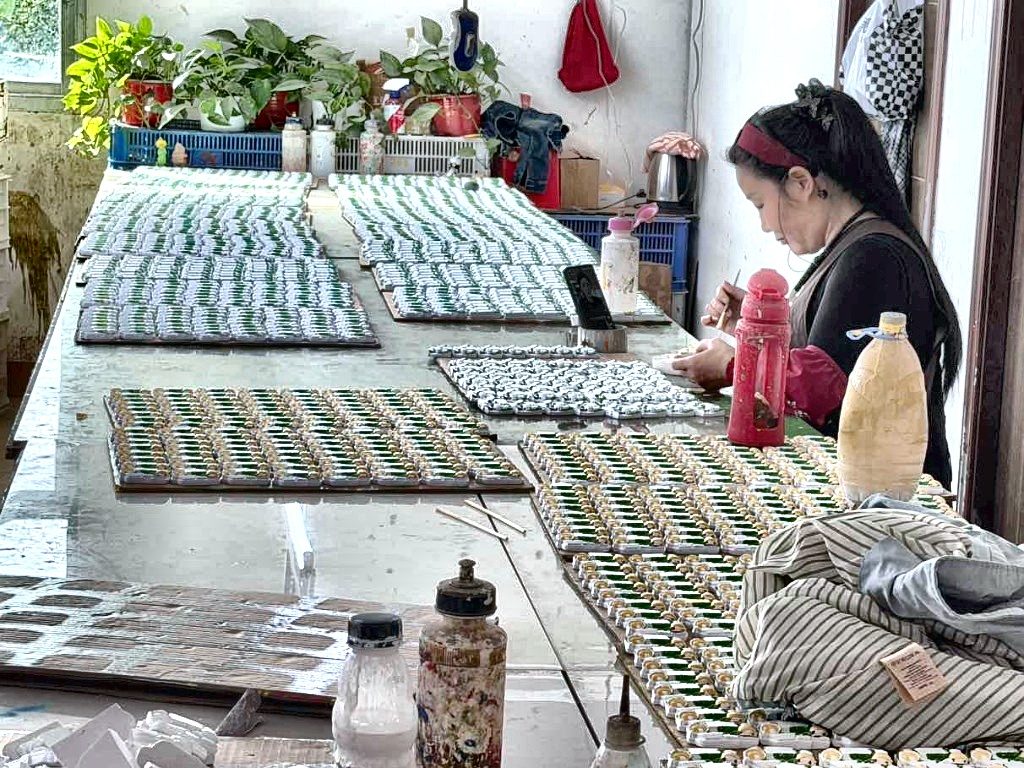
Two years ago, an executive vice president from a major collectible gaming merchandise publisher in Los Angeles flew unannounced to our Quanzhou factory. He laid five thousand painted dragon figurines onto our boardroom conference table. They had been produced by a low-cost competitor in a neighboring province. At first glance under showroom spotlights, the figurines looked dramatic and detailed. But under 10x inspection loupes, the disaster became apparent: across the dragon's nose ridge, horned crests, and underbelly scales, hundreds of microscopic pits—measuring between 0.15mm and 0.40mm in diameter—had formed small craters. In the competitor's workshop, operators had attempted to disguise these surface bubbles by smearing cheap polyester automotive body-putty across the raw castings before sending them to the paint booth. Within ninety days of ocean container transport through warm Pacific waters, the residual styrene in the resin outgassed, the putty shrank, and the topcoat cracked into unsightly pinhole craters. The client was facing an inventory write-down exceeding $140,000.
During my twenty-six years managing resin casting cells, silicone mold bays, and robotic slurry dispensers here at ArtisResin Craft Co., Ltd., I have drilled one cardinal rule into our tooling team: a bubble is an engineering failure that must be eliminated in the liquid phase; it can never be cured with a putty knife. Patching pinholes is a fraudulent band-aid that invariably fails when the product encounters fluctuating ambient temperature and humidity. In this engineering guide, I will detail the thermodynamic, rheological, and mechanical systems ArtisResin uses to achieve 99.9% bubble-free castings across millions of high-detail polyresin figurines, statues, and home accents.
1. The Fluid Physics of Bubble Entrapment: Stokes' Law vs. Slurry Viscosity
To understand why air bubbles refuse to escape from polyresin naturally, procurement engineers must examine the fluid dynamics of heavily filled polymer slurries. When high-grade unsaturated polyester resin is blended with 60% ground calcium carbonate, dolomite flour, or atomized bronze powder, the fluid ceases to behave like water (which has a dynamic viscosity of 1 cP). Instead, it behaves as a non-Newtonian pseudoplastic slurry with an apparent dynamic viscosity ranging between 1,800 and 2,800 centipoise (cP) at 25°C.
The natural buoyant ascent velocity of a trapped spherical air bubble through a stationary liquid column is governed strictly by Stokes' Law:
vt = (2 · g · r² · (ρliquid - ρgas)) / (9 · η)
where:
- g is gravitational acceleration (9.81 m/s²)
- r is the bubble radius (meters)
- ρliquid is resin slurry density (1,780 kg/m³)
- ρgas is air density (1.2 kg/m³)
- η is dynamic viscosity (2.2 Pa·s)
Let us calculate the escape velocity of a typical 0.2 mm diameter (r = 0.0001 m) pinhole bubble in an un-degassed casting slurry:
In a standard polyresin sculpture with a wall thickness of 35mm, that 0.2mm bubble would require more than thirty-three minutes to float to the open top of the mold. However, commercial polyester resin formulated with methyl ethyl ketone peroxide (MEKP) catalysts has a working gelation window (pot life) of only twelve to eighteen minutes at standard workshop temperatures. Long before the micro-bubble can reach the surface, the liquid resin cross-links into a solid gel, locking millions of microscopic voids permanently inside the body and against the silicone cavity walls.
2. Dual-Stage Industrial Vacuum Degassing Engineering (-0.095 MPa Protocol)
Because gravity alone cannot overcome viscous resistance within the available gelation time, ArtisResin deploys deterministic negative-pressure physics governed by Boyle's Ideal Gas Law (P1V1 = P2V2). When ambient pressure surrounding an air bubble is dropped from 101.3 kPa (atmospheric) down to 5.0 kPa absolute pressure (-0.095 MPa gauge vacuum), the physical volume of every trapped air bubble expands by a factor of more than twenty:
V2 / V1 = P1 / P2 = 101.3 kPa / 5.0 kPa = 20.26× Volumetric Expansion
Because volume scales with radius cubed (V ∝ r³), the effective bubble radius expands by √[3](20.26) = 2.73×.
According to Stokes' Law, buoyant velocity scales with r²: (2.73)² = 7.45× Faster Ascent Velocity!
Under this dramatic expansion, micro-bubbles swell into massive buoyant pockets that surge violently toward the liquid surface. Our proprietary Dual-Stage Vacuum Degassing Protocol operates as follows:
- Stage 1: Bulk Reactor Vacuum De-Aeration: Immediately following high-shear mechanical dispersion of fillers and pigments, 200-liter batches of resin are sealed inside our heavy ASME-certified stainless steel vacuum kettles. Two dual-stage oil-sealed rotary vane pumps pull vacuum down to -0.095 MPa in under 45 seconds. The resin slurry boils violently, rising up to 2.5 times its static liquid level in a frothy foam head. As the giant expanded bubbles reach the liquid-gas interface, their thin wall membranes burst, venting the trapped air into the vacuum pump exhaust. After 180 seconds of boiling, an automated solenoid valve momentarily pulses atmospheric air back into the chamber, imploding any remaining micro-bubbles and returning the liquid to an ultra-dense, void-free optical state.
- Stage 2: Differential Vacuum-Assisted Cavity Infiltration: Even with pristine liquid resin, pouring into intricate mold geometries at atmospheric pressure can trap air in blind recesses (such as down-facing fingertips, nostrils, or under-cut feathers). To ensure 100% surface wetting, our technicians place the filled platinum silicone molds inside secondary vacuum autoclaves. Negative pressure of -0.085 MPa is applied for 90 seconds while an electromagnetic vibration table oscillates the molds at 50 Hz with an amplitude of 0.25mm. The vibration breaks liquid surface tension against the silicone walls, causing any clinging bubbles to detach and float upward into the overflow reservoir.
3. Silicone Tooling Elastomer Chemistry: Platinum (Addition) vs. Tin (Condensation)
Vacuum degassing liquid resin is only half the battle. If the flexible mold itself outgasses volatile chemical compounds during the exothermic cure of the resin, surface pinholes will continuously regenerate at the mold-substrate boundary. In the Chinese polyresin manufacturing sector, over 70% of low-tier workshops continue to build molds using cheap condensation-cure (tin-catalyzed) silicone rubbers due to their low cost ($4.50/kg vs $11.00/kg for platinum silicone).
Tin-cure silicones cure through a condensation reaction between hydroxyl-terminated polydimethylsiloxane and tetraalkoxysilanes in the presence of dibutyltin dilaurate. This reaction inevitably releases ethyl alcohol or acetic acid as volatile byproducts. These solvent molecules remain trapped inside the porous silicone matrix. When warm polyester resin is poured into a tin-cure mold, the exothermic reaction heat (often reaching 110°C) causes the residual alcohol to flash-boil into vapor at the mold surface, creating a continuous carpet of tiny micro-pinholes known as 'tooling boil.' Furthermore, tin-cure silicones suffer high linear shrinkage (0.4% to 0.8% over 72 hours), distorting fine geometric dimensions.
ArtisResin mandates 100% addition-cure (platinum-catalyzed) vinyl polysiloxane silicone for all production tooling. Platinum silicones cross-link via hydrosilylation: vinyl groups (CH=CH2) react cleanly with silicon-hydride (Si-H) bonds in the presence of a Karstedt platinum catalyst. There are zero volatile reaction byproducts. Linear shrinkage is virtually undetectable (< 0.05% across a 500mm span). Below is our certified tooling selection matrix based on product geometric complexity:
| Tooling Parameter | Low-Cost Condensation Silicone (Tin-Cure) | ArtisResin Platinum Silicone (Shore A 28) | ArtisResin High-Tear Platinum (Shore A 22) |
|---|---|---|---|
| Catalyst Chemistry | Dibutyltin Dilaurate (Toxic Tin Salts) | Platinum Complex (Organometallic Pt) | Platinum Complex (Branched Siloxane) |
| Volatile Reaction Byproducts | Ethanol / Acetic Acid (Causes Pinholes) | Zero Byproducts (Pure Addition) | Zero Byproducts (Pure Addition) |
| Linear Vulcanization Shrinkage | 0.45% – 0.80% (Dimensional Drift) | ≤ 0.05% (CAD Precision True) | ≤ 0.08% (Ultra-Low Shrinkage) |
| Tensile Strength (ASTM D412) | 3.2 MPa | 6.8 MPa (+112% Tougher) | 5.5 MPa |
| Tear Propagation Strength (ASTM D624 Die B) | 14.0 kN/m (Tears Easily on Undercuts) | 28.5 kN/m (Superior Tear Resistance) | 32.0 kN/m (Extreme Undercut Resilience) |
| Elongation at Break | 280% ± 30% | 480% ± 40% | 620% ± 50% (Extreme Elasticity) |
| Useful Demolding Cycles per Cavity | 60 – 85 Pulls | 180 – 220 Pulls (+160% Life) | 150 – 190 Pulls |
| Surface Pinhole Rejection Rate | 8.5% – 14.2% Scrap Rate | < 0.2% First-Pass Defect | < 0.3% First-Pass Defect |
4. CAD-Engineered Riser Venting & Micro-Parting Line Optimization
Even with vacuum-degassed resin and outgas-free platinum silicone, mechanical air entrapment can still occur if mold cavity ventilation is improperly routed. In conventional mold making, mold technicians cut crude vent slits into silicone parting lines with razor blades. These hand-cut slits vary in depth, frequently clog with cured resin flash, and leave thick witness marks (flash lines) requiring aggressive manual grinding that destroys sculptured surface details.
In ArtisResin's computerized tooling division, our CAD mold engineers run digital mold-flow simulations in Siemens NX Mold Wizard prior to cutting silicone mother molds. We identify all geometric 'dead-end high points'—such as the tips of raised animal ears, the peak of an outstretched sword, or deep drapery folds. We then design engineered 2.5mm conical runner vents (risers) that lead directly from these high points to external atmospheric vent cups. When liquid resin fills the silicone cavity under vacuum vibration, the rising fluid front drives all remaining air ahead of it, venting through the risers until liquid resin overflows into the vent cup. This guarantees 100% complete cavity filling with zero blind air locks.
Furthermore, we engineer stepped, interlocking silicone parting lines with tongue-and-groove registration keys. When the multi-piece silicone core is assembled inside its rigid fiberglass mother shell (jacket), the silicone edges compress under a calibrated 0.8 mm interference fit. This eliminates liquid resin seepage along parting lines, keeping parting flash thickness below 0.08mm. Technicians can dress the minimal parting flash using a single stroke of 600-grit micro-abrasive film, leaving the adjacent sculptured texture completely untouched.
ArtisResin verifies internal structural density on every production lot using ASTM D2734 (Standard Test Methods for Void Content of Reinforced Plastics). Certified production specimens must demonstrate a calculated void content of less than 0.15% by total volume. Furthermore, surface pinhole density is audited across fifty randomly sampled units per container lot using an Olympus digital stereomicroscope under 20x magnification. The quality gate is uncompromising: zero pinholes greater than 0.10mm on prominent focal faces, and an overall surface defect density under 0.2 defects per 100 cm².
6. Combined Hyperbaric Pressure Pot Curing (0.45 MPa Protocol)
While negative-pressure vacuum degassing eliminates 99.8% of micro-bubbles in the liquid slurry prior to pouring, certain extreme sculptural geometries featuring blind micro-crevices (such as 0.15mm filigree engraving, pierced lace filigree on figurines, or deep recessed ear canals) can occasionally shelter microscopic air caps during fluid entry. To achieve absolute perfection on museum-grade and high-end collectible prototypes, ArtisResin pairs liquid vacuum degassing with a secondary post-pour hyperbaric pressure pot cure cycle.
Immediately after pouring vacuum-degassed resin into the platinum silicone mold, the entire mold assembly is loaded inside an ASME-certified pneumatic pressure vessel. The chamber is sealed and charged with clean, dry compressed air up to a working pressure of 0.45 MPa (65 psi). Under this intense external positive pressure, Boyle's Ideal Gas Law operates in reverse: any microscopic air bubbles remaining in the liquid resin are physically compressed down to less than one-fiftieth of their original volume. The micro-bubbles become physically microscopic (smaller than 5 microns in diameter), forcing them into total chemical solution within the liquid polyester resin matrix. The resin is held under continuous 0.45 MPa pressure until the exothermic polymerization reaches its peak and the resin transitions into a glassy, fully cross-linked solid state. When the pressure vessel is depressurized, the cured resin retains its flawless, void-free optical density. This dual-action thermodynamic combination of pre-pour vacuum degassing (-0.095 MPa) followed by in-mold hyperbaric pressure curing (0.45 MPa) guarantees that zero voids or surface pinholes can physically exist on the finished collectible sculpture.
5. Troubleshooting Common Casting Defects: Factory Floor SOP
When our engineers conduct audits of struggling manufacturing workshops, we utilize the following diagnostic root-cause matrix to identify and correct liquid casting flaws:
- Defect Symptom 1: Clustered Pinholes on Upper Surface Peaks.
- Root Cause: Insufficient vacuum degassing time or failure to provide upward riser vents on geometric dead ends. Air is trapped as the fluid front converges.
- Engineering Countermeasure: Extend vacuum boiling time under -0.095 MPa from 120s to 180s. Add a 2.5mm silicone riser vent at the highest peak connecting to the exterior overflow cup.
- Defect Symptom 2: Universal Foamy Sponge-Like Porosity Throughout Core.
- Root Cause: High moisture contamination in the calcium carbonate or mineral filler. Water reacts chemically with isocyanates (in polyurethane resins) or inhibits polyester cross-linking, boiling during exothermic cure.
- Engineering Countermeasure: Mandate raw filler drying ovens operating at 105°C for 4 hours prior to slurry compounding. Verify filler moisture content is below 0.05% using a Karl Fischer titrator.
- Defect Symptom 3: Blisters Forming 30 to 90 Days After Painting.
- Root Cause: Manual cosmetic patching using polyester car putty over untreated pinholes. Putty absorbs atmospheric humidity through paint films, swelling and delaminating.
- Engineering Countermeasure: Ban all manual putty patching on the factory floor. Reject any casting with surface voids exceeding 0.15mm and recycle through crushing into non-structural core ballast.
Frequently Asked Tooling Questions from Sourcing Managers
Q1: Why does ArtisResin require a 5 to 7 day lead time for custom prototype molds when some factories promise 48 hours?
A: Rushing silicone vulcanization requires adding excess chemical accelerators or using cheap tin catalysts, which causes high shrinkage (0.8%) and severe outgassing pinholes. At ArtisResin, we cure our platinum silicone under temperature-controlled 25°C chambers for a full 24 hours, followed by a secondary post-cure bake at 60°C for four hours. This ensures complete chemical cross-linking, zero volatile emissions, and microscopic ±0.05mm dimensional fidelity.
Q2: How many pieces can be produced from a single silicone mold cavity before detail degrades?
A: For standard stone-powder polyresin, our Shore A 28 platinum silicone molds deliver 180 to 220 clean demolding cycles. For heavy cold cast bronze loaded with 70% abrasive bronze metal powder, mold life is approximately 140 to 160 cycles. When quoting custom OEM programs, we calculate exact mold cavity multiples to guarantee that fresh, sharp tooling is running throughout the entire purchase order.
Q3: How can we specify zero-pinhole quality in our formal OEM purchase orders?
A: We recommend including this specific clause in your Quality Agreement: 'Casting shall be manufactured via -0.095 MPa vacuum degassing in addition-cure platinum silicone tooling. Internal void content shall be < 0.15% per ASTM D2734. Surface pinholes > 0.10mm on Grade A aesthetic surfaces shall be zero. Downstream patching with automotive polyester filler is strictly prohibited.' ArtisResin contractually guarantees compliance with this standard on every commercial shipment.
7. Platinum-Catalyzed Addition-Cure vs. Tin-Cure Shrinkage Fatigue & Multi-Part Undercut Tooling Lifecycles
In industrial polyresin reproduction, mold tooling degradation directly governs production unit costs, dimensional repeatability, and surface micro-texture retention. Standard commercial artisan shops predominantly rely on condensation-cure (tin-catalyzed) silicone rubbers due to their initial cost advantage (approximately 45% cheaper per kilogram of RTV elastomer). However, tin-cure formulations liberate ethyl alcohol or acetic acid as volatile condensation byproducts during vulcanization, causing progressive volumetric linear shrinkage of 0.35% to 0.65% over a 30-day operational window. In high-precision commercial figurine editions where multi-component sub-assemblies (such as interchangeable weapon parts, modular stone plinths, or interlocking magnetic wings) must seat within 0.12 mm mechanical tolerances, tin-cure shrinkage inevitably triggers catastrophic batch misalignments.
ArtisResin mandates two-component addition-cure (platinum-catalyzed) polyorganosiloxane liquid rubbers exclusively for all OEM/ODM master production runs. Platinum-catalyzed cross-linking proceeds via hydrosilylation without producing volatile reaction byproducts, maintaining an absolute linear shrinkage rate under 0.04% over 365 days of continuous factory climate cycling (22°C, 50% relative humidity). Furthermore, our tooling engineers custom-blend Shore A 28 durometer base rubber with 12% vinyl-terminated silicone plasticizer oil, engineering a superior elongation-at-break of 520% and an exceptional tear strength of 28 kN/m (tested to ASTM D624 Die B).
This high-elasticity formulation permits single-piece glove mold configurations with extreme negative draft angles and dramatic undercuts of up to 48 degrees, eliminating the necessity of intrusive multi-part parting lines across facial contours, hair locks, or delicate lacework. To mitigate silicone poisoning risks inherent to platinum catalysts (inhibition triggered by residual sulfur in modeling clays, amine hardeners, or organotin compounds), our master patterns are coated with a dual-layer sacrificial barrier consisting of micronized polyvinyl alcohol (PVA) film followed by baked fluoropolymer mold release. The realized tooling lifecycle reaches 120 to 150 defect-free resin cast cycles per mold cavity prior to elastomeric fatigue, compared to merely 35 to 45 pulls typical of unreinforced tin-cure alternatives, providing significant amortized cost savings on high-volume holiday and retail tabletop programs.